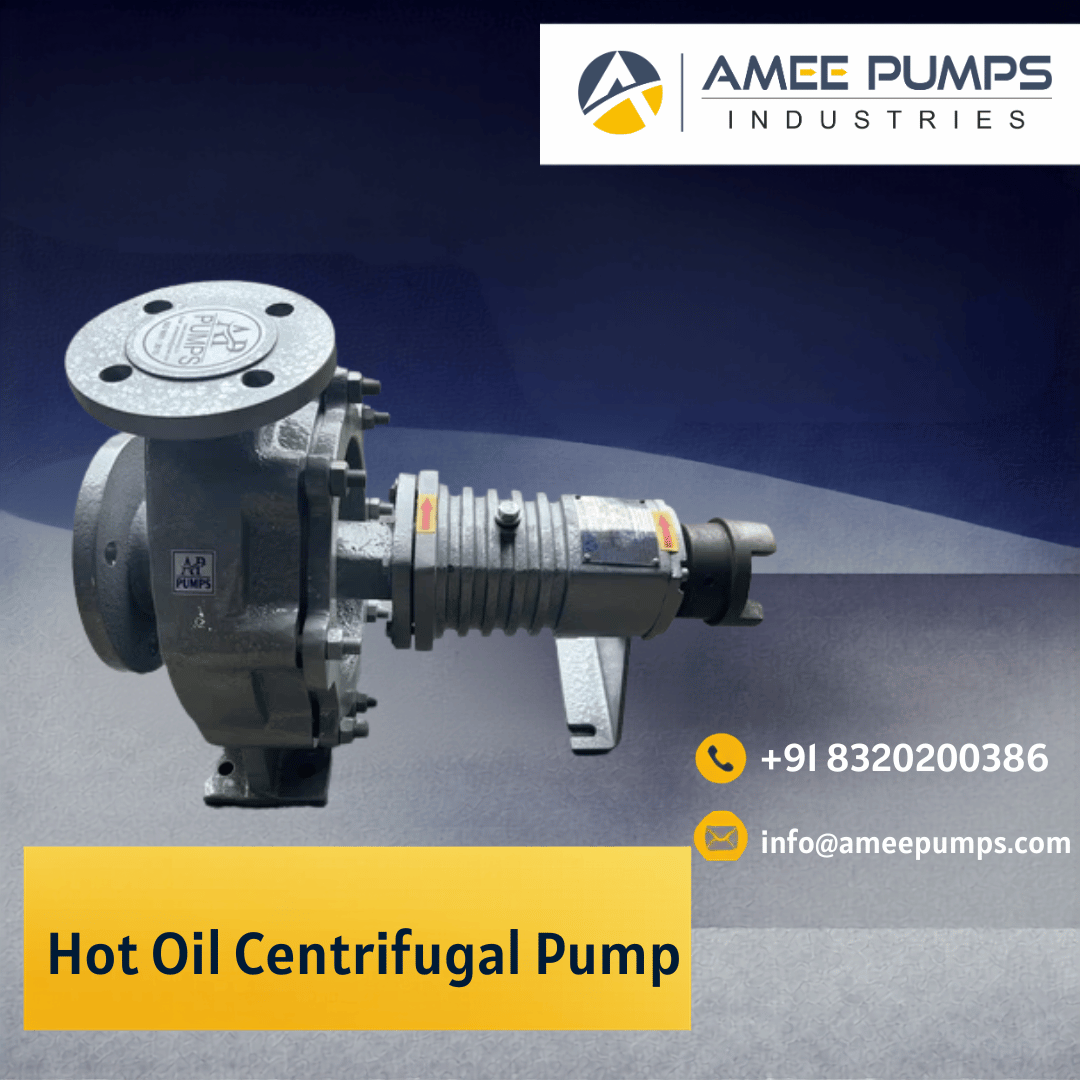
Hot Oil Centrifugal Pump
In industrial processes requiring precise temperature control, the reliable circulation of high-temperature thermal fluids is paramount. Hot oil centrifugal pumps are the backbone of these systems, ensuring uniform heat distribution and efficient operation. AMEE PUMPS INDUSTRIES specializes in manufacturing robust and efficient hot oil centrifugal pumps designed to meet the demanding requirements of various industries.
These specialized pumps are engineered to handle thermal oils at elevated temperatures, making them indispensable for applications where consistent heating is crucial. Understanding their functionality, benefits, and selection criteria is key to optimizing your industrial heating processes.
Understanding Hot Oil Centrifugal Pumps
A hot oil centrifugal pump is a type of positive displacement pump specifically designed for circulating high-temperature thermal oils (also known as heat transfer fluids) within closed-loop industrial heating systems. Unlike standard centrifugal pumps, these units are built with specialized materials and design considerations to withstand the extreme thermal conditions and the unique properties of thermal oils.
The primary function of a hot oil centrifugal pump is to ensure the continuous and stable flow of heated oil from a boiler or heater to various process equipment, and then back to the heater for reheating. This creates a closed-loop system that maintains a consistent and controllable temperature across the entire industrial process, which is vital for product quality, process efficiency, and energy conservation.
Operating on the centrifugal principle, these pumps utilize an impeller to impart kinetic energy to the fluid, converting it into pressure energy to move the oil through the system. This method ensures a smooth, uninterrupted flow, preventing the localized overheating or cooling that could occur with less sophisticated pumping mechanisms.
Key Applications of Hot Oil Centrifugal Pumps
The versatility and reliability of hot oil centrifugal pumps make them essential in a wide array of industrial sectors. Their ability to maintain precise temperatures and handle demanding fluids ensures efficient performance across various critical applications:
Chemical Processing
Used for heating reactors, distillation columns, and other process vessels requiring stable, high-temperature environments for chemical reactions.
Textile Industry
Essential for heating dye vats, drying ovens, and continuous processing lines where uniform heat application is critical for fabric treatment.
Pharmaceuticals
Employed in sterilization processes, drying operations, and maintaining precise temperatures for sensitive drug manufacturing stages.
Food Processing
Utilized in industrial ovens, fryers, and cooking equipment that rely on stable thermal oil circulation for consistent product quality.
Rubber Manufacturing
Crucial for heating presses, curing equipment, and calendering machines to ensure proper vulcanization and material processing.
Wood Processing
Used in heated presses for laminating, drying kilns, and other applications requiring controlled high-temperature heat transfer.
Key Features and Practical Benefits
Hot oil centrifugal pumps from AMEE PUMPS INDUSTRIES are engineered with robust features to deliver exceptional performance and reliability. These characteristics translate into significant practical benefits for your operations:
Design Features
- High-Temperature Operation: Capable of handling thermal oils up to 300°C, with models suitable for 200°C and 250°C, ensuring compatibility with a wide range of heating systems.
- Robust Construction: Built with durable materials like cast iron and specialized stainless steel alloys to withstand extreme thermal stress and resist corrosion.
- Advanced Sealing: Utilizes high-temperature mechanical seals specifically designed to prevent leakage of hot thermal fluids, ensuring safety and operational integrity.
- Efficient Flow: Centrifugal design provides smooth, continuous, and uninterrupted circulation of thermal oil, maintaining uniform temperature distribution.
- Air Cooled Options: Available as Air Cooled Thermic Fluid Pumps, eliminating the need for external water cooling systems and simplifying installation and maintenance.
Operational Benefits
- Improved Process Efficiency: Consistent temperature control across the system minimizes energy losses and enhances overall process output.
- Reduced Downtime: Low maintenance requirements and high reliability, owing to robust construction and minimized wear, lead to longer service life and fewer interruptions.
- Enhanced Safety: Effective sealing technologies and sturdy build quality significantly reduce the risk of leaks and thermal fluid degradation, ensuring a safer working environment.
- Precise Temperature Management: Guarantees uniform heat transfer, crucial for maintaining product quality and consistency in sensitive manufacturing processes.
- Simplified System: Air-cooled variants reduce the complexity of auxiliary cooling infrastructure.
Selecting Your Hot Oil Centrifugal Pump
Choosing the right hot oil centrifugal pump is critical for the efficiency, safety, and longevity of your industrial heating system. Consider the following factors when making your selection:
Essential Selection Criteria
- Temperature Requirements: Ensure the pump's maximum operating temperature significantly exceeds your system's highest expected thermal oil temperature. AMEE PUMPS INDUSTRIES offers models up to 300°C.
- Flow Rate & Head: Determine the required flow rate (m³/hr) and system head pressure. Pumps are available with capacities up to 500 m³/hr.
- Fluid Compatibility: Confirm the pump materials and seals are compatible with the specific type of thermal oil being used, considering its viscosity and chemical properties at operating temperatures.
- System Design: Whether an air-cooled or a traditional fluid-cooled system is more suitable for your installation constraints and operational needs.
- Reliability and Maintenance: Opt for pumps known for low maintenance and high reliability, such as those constructed with durable materials and featuring proven sealing technologies.
- Manufacturer Support: Partner with a reputable manufacturer like AMEE PUMPS INDUSTRIES that offers expertise and a commitment to quality.
Buyer Insight
Always consult with the pump manufacturer's technical team to ensure the selected pump precisely matches your system's unique operating parameters and safety requirements. Understanding your system's flow dynamics and thermal load is crucial for optimal pump sizing.
AMEE PUMPS INDUSTRIES: Your Partner for Hot Oil Circulation
Established in 2009 and based in Ahmedabad, Gujarat, India, AMEE PUMPS INDUSTRIES has dedicated itself to providing high-quality pumping solutions. With a focus on specialized industrial pumps, including robust hot oil centrifugal pumps, the company has built a reputation for reliability and performance.
AMEE PUMPS INDUSTRIES offers hot oil centrifugal pumps designed for efficient circulation of high-temperature thermal oils. Their range includes models capable of handling diverse capacities and temperatures, up to 500 m³/hr and up to 300°C respectively. The company also provides innovative solutions like Air Cooled Thermic Fluid Pumps that simplify system design. Committed to excellence, AMEE PUMPS INDUSTRIES strives to ensure operational efficiency and minimal downtime for its clients across various demanding industrial sectors.
Frequently Asked Questions
What is the primary function of a hot oil centrifugal pump?
The primary function is to continuously circulate high-temperature thermal oils within industrial heating systems, ensuring uniform heat distribution and maintaining precise process temperatures.
What temperatures can these pumps handle?
AMEE PUMPS INDUSTRIES' hot oil centrifugal pumps can handle temperatures up to 200°C, with some models suitable for up to 250°C or 300°C, depending on the specific design.
Are there any advantages to air-cooled thermic fluid pumps?
Yes, air-cooled thermic fluid pumps eliminate the need for external water cooling systems, simplifying installation, reducing water consumption, and lowering maintenance requirements.
What industries commonly use hot oil centrifugal pumps?
Common industries include chemical processing, textiles, pharmaceuticals, food processing, rubber manufacturing, and wood processing, where controlled high-temperature heating is essential.
How do I choose the right hot oil centrifugal pump for my application?
Key considerations include the required temperature range, flow rate, system head pressure, fluid compatibility, and whether an air-cooled or traditional system is more appropriate. Consulting with the manufacturer is highly recommended.
Ready to Optimize Your Heating System?
Ensure your industrial processes benefit from reliable, efficient, and safe thermal fluid circulation. Contact AMEE PUMPS INDUSTRIES today to discuss your specific requirements and find the perfect Hot Oil Centrifugal Pump solution for your operational needs.
Explore AMEE PUMPS Solutions