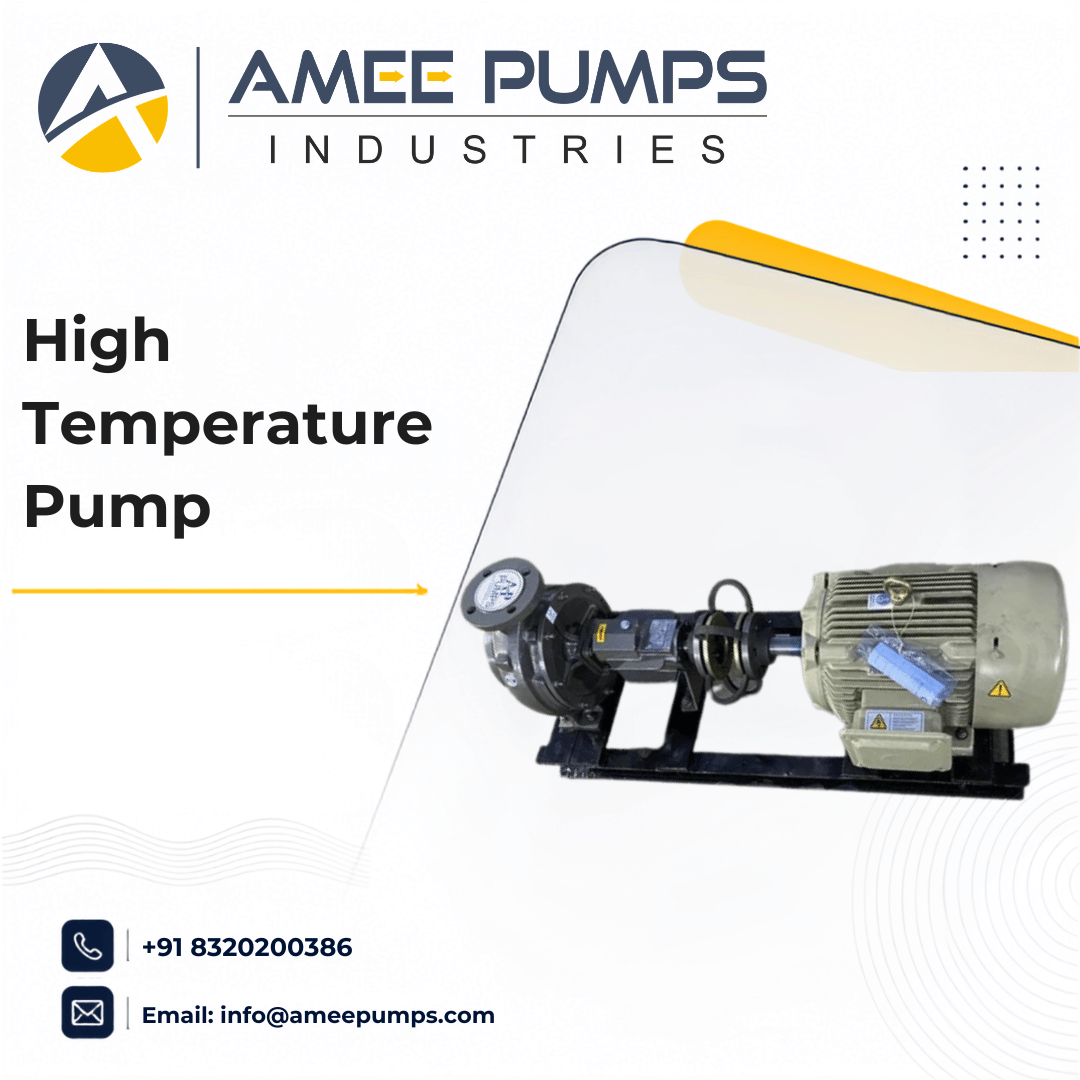
High Temperature Pump
High-temperature pumps are indispensable components in a vast array of industrial processes, designed to handle fluids that operate well beyond standard ambient conditions. These specialized machines are engineered to maintain their operational integrity and efficiency under extreme thermal stress, ensuring continuity and safety in demanding environments. From chemical manufacturing to thermal power generation, the reliability of a high-temperature pump directly impacts process efficiency and operational success.
AMEE PUMPS INDUSTRIES, established in 2009 and guided by the extensive experience of Mr. Amit Panchal, offers a tech-driven approach to designing and manufacturing pumps that meet these rigorous requirements. With a commitment to precision and cost-effectiveness, the company provides solutions for handling challenging high-temperature liquids, ensuring performance where standard pumps would fail.
Understanding High Temperature Pumps
High-temperature pumps are specifically engineered to operate reliably with fluids that are heated to elevated temperatures, often exceeding 200-250 degrees Celsius, and in some cases, up to 350°C. The primary challenge in designing these pumps lies in their ability to withstand thermal expansion, maintain seal integrity, and prevent material degradation under continuous high heat. Typical construction materials include robust cast iron or specialized stainless steel alloys, chosen for their thermal stability and resistance to corrosion at high temperatures.
Advanced sealing technologies, such as high-temperature mechanical seals, are crucial to prevent leakage and ensure safe operation. These pumps are vital for applications involving thermic fluid circulation, chemical transfer at elevated temperatures, boiler feed processes, and managing hot water systems in various industrial settings.
Key Applications and Use Cases
The versatility of high-temperature pumps makes them suitable for a broad spectrum of industrial operations:
Thermic Fluid Systems
Circulating hot oils and thermal fluids used for heating in manufacturing processes.
Chemical Processing
Transferring aggressive chemicals and intermediates that require elevated temperatures for reactions or to maintain viscosity.
Manufacturing Facilities
Supporting various heating and cooling cycles in industrial production lines.
Boiler Feed Processes
Supplying high-temperature water or steam to boilers, crucial for power generation and industrial heating.
Hot Water Systems
Circulating hot water in large-scale heating systems and industrial processes.
Advantages of Using High-Performance Pumps
Investing in the right high-temperature pump offers significant operational advantages:
- Enhanced Process Efficiency: Maintain optimal operating temperatures for critical processes, leading to improved product quality and reduced processing times.
- Reliable Operation: Robust construction and specialized sealing technology minimize downtime and ensure consistent performance even under harsh conditions.
- Safety and Environmental Protection: High-integrity seals prevent hazardous fluid leaks, safeguarding personnel and the environment.
- Durability and Longevity: Made with materials suited for high heat, these pumps offer extended service life, reducing the total cost of ownership.
- Versatility: Adaptable to a wide range of high-temperature liquid handling tasks across various industries.
Selecting the Right High Temperature Pump
Choosing an appropriate high-temperature pump requires careful consideration of several factors to ensure optimal performance and longevity. AMEE PUMPS INDUSTRIES emphasizes a practical approach, focusing on the specific demands of your application.
Buyer Insight
When evaluating high-temperature pumps, prioritize the pump's ability to consistently perform at elevated temperatures. Consider the construction materials' compatibility with the fluid being handled and the reliability of the sealing mechanism. Understanding the specific industrial process and its unique thermal challenges is key to selecting a pump that offers both efficiency and long-term durability.
Key Selection Criteria:
Material Compatibility
Ensure the pump's materials (e.g., cast iron, stainless steel) are resistant to corrosion and degradation at the operating temperature and in contact with the specific fluid.
Temperature Rating
Verify that the pump's design and materials can safely and reliably handle the maximum operating temperature, including potential temperature fluctuations.
Sealing Technology
Evaluate the type and quality of the mechanical seal or gland packing. High-temperature applications demand robust sealing solutions to prevent leaks and ensure safety.
Application Suitability
Consider the fluid's viscosity, solids content, and any abrasive properties, alongside the required flow rate and head, to match the pump type (e.g., centrifugal, gear) to the task.
Maintenance and Serviceability
Opt for pumps designed for ease of maintenance, especially in hard-to-access locations or continuous operation scenarios.
Efficiency and Energy Consumption
Look for pumps that offer good hydraulic efficiency at your operating point to minimize energy costs over the pump's lifetime.
Questions to Ask Before Buying:
What is the maximum continuous operating temperature the pump can handle?
Confirm the pump's sustained temperature capability to avoid premature failure or performance degradation.
What materials are used in the pump's construction and seals?
Understand the materials' suitability for your specific fluid and operating temperature to ensure chemical compatibility and thermal resistance.
Does the pump require special installation or startup procedures for high-temperature fluids?
Inquire about any specific requirements for safe and efficient installation and initial operation.
What is the expected lifespan and maintenance schedule for the pump under high-temperature conditions?
Gain insight into the pump's durability and the ongoing service requirements to budget effectively.
AMEE PUMPS INDUSTRIES: Your Partner for High Temperature Pumping Solutions
Established in 2009 and rooted in Ahmedabad, Gujarat, AMEE PUMPS INDUSTRIES, under the leadership of Mr. Amit Panchal, brings over two decades of industry expertise to the design and manufacturing of specialized pumps. The company leverages a technology-driven approach to develop high-performance pumping solutions, focusing on precision engineering and cost-effectiveness. Their commitment to a 100% success rate on projects underscores their dedication to delivering reliable and efficient outcomes for their clients.
AMEE PUMPS INDUSTRIES offers a range of Chemical Process Pumps specifically designed to handle demanding high-temperature applications, capable of managing fluids up to 200-250 degrees Celsius. This capability, combined with their diverse product line including specialized pumps like Magnetic Drive Pumps and Vertical Seal/Gland Less Pumps, positions them as a capable provider for industries requiring robust solutions for extreme thermal conditions.
Frequently Asked Questions
What distinguishes a high-temperature pump from a standard industrial pump?
High-temperature pumps are constructed with specialized materials and advanced sealing technologies to withstand continuous operation at elevated fluid temperatures, whereas standard pumps are designed for ambient or moderately heated fluids.
Can AMEE PUMPS INDUSTRIES provide solutions for temperatures exceeding 250°C?
AMEE PUMPS INDUSTRIES offers Chemical Process Pumps capable of handling temperatures up to 200-250 degrees Celsius, aligning with specific industrial needs for high-temperature fluid transfer.
What are the common failure points for pumps operating at high temperatures?
Common failure points include mechanical seal degradation, material distortion or failure due to thermal stress, and overheating of bearings or motor components. Proper material selection and robust sealing are key to prevention.
Are self-priming features available on high-temperature pumps?
While not all high-temperature pumps are self-priming, this feature can be beneficial for easier startup and operation, especially in systems where the pump may lose its prime. It helps in evacuating air from the suction line.
Ready to Meet Your High Temperature Pumping Needs?
Ensure your industrial processes run smoothly and safely with reliable high-temperature pumps. Contact AMEE PUMPS INDUSTRIES today to discuss your specific application requirements and discover tailored solutions engineered for performance and durability.
Request a Consultation