Centrifugal Couple Drive Chemical Process Pump
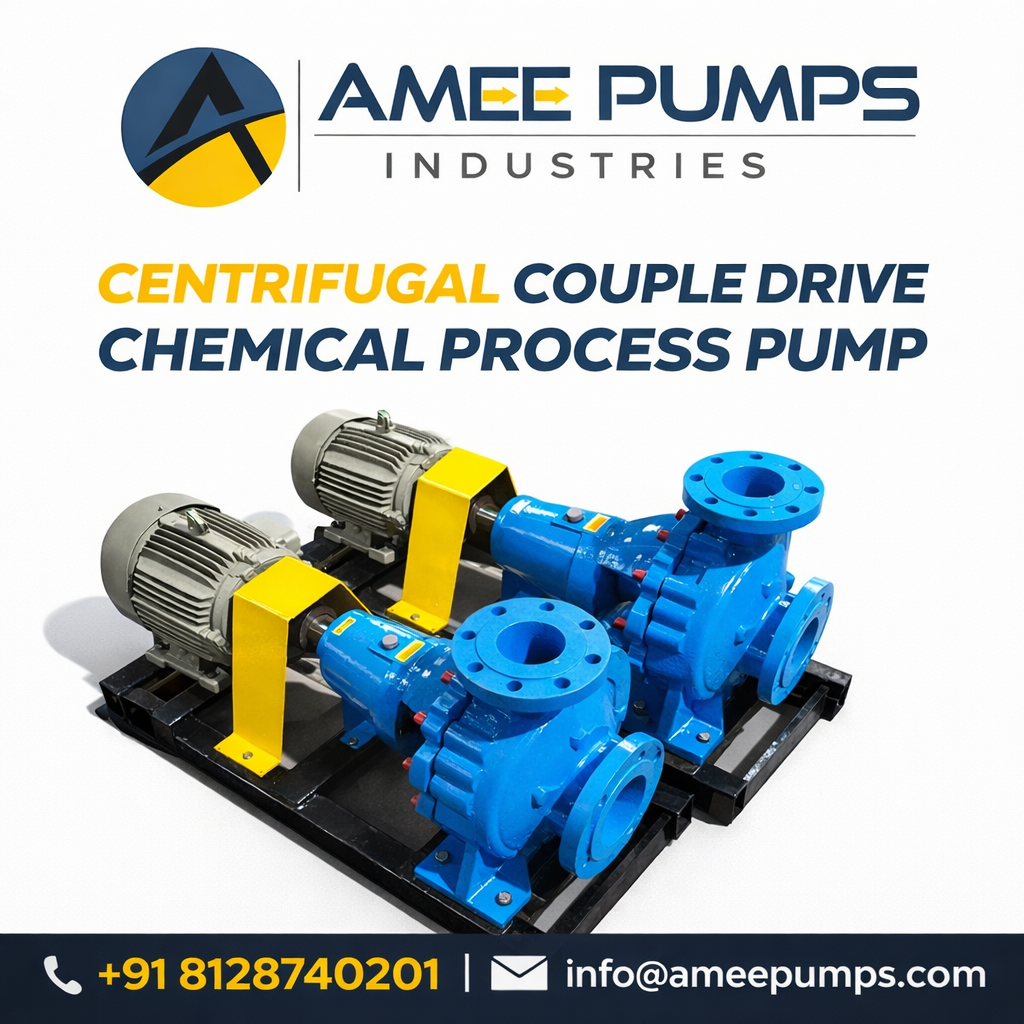
Centrifugal Couple Drive Chemical Process Pump
Industrial fluid handling systems rely on dependable pumping equipment to move liquids efficiently between different stages of production. A centrifugal couple drive chemical process pump is designed to transfer chemical fluids safely while maintaining operational stability in demanding industrial environments. These pumps play a critical role in industries where corrosive liquids, reactive chemicals, or process fluids must be transported continuously without compromising system integrity.
Unlike general-purpose pumps, chemical process pumps are engineered with specialized materials and design features that allow them to operate reliably under challenging conditions. Chemical processing facilities, manufacturing plants, and industrial treatment systems require pumping equipment capable of handling aggressive fluids while maintaining consistent flow rates. A centrifugal couple drive chemical process pump fulfills this requirement through a robust design that supports stable and reliable fluid transfer.
As industrial operations become more complex and production demands continue to increase, the need for dependable pumping systems grows. Chemical processing industries rely on pumps that combine efficiency, durability, and consistent performance. Centrifugal couple drive chemical process pumps have become a preferred solution because they support continuous operation while helping minimize operational disruptions.
Understanding Centrifugal Couple Drive Chemical Process Pump Technology
A centrifugal couple drive chemical process pump operates using centrifugal force to move liquids through a piping system. The pump consists of an impeller mounted directly on the motor shaft, which rotates at high speed to generate the energy required to move fluids.
When the impeller rotates, liquid enters the pump through the suction inlet and is accelerated outward by the impeller blades. The centrifugal force generated by this motion increases the velocity of the liquid, converting mechanical energy into fluid energy. As the fluid moves through the pump casing, the velocity is transformed into pressure, allowing the liquid to be transported through pipelines to the next stage of processing.
The couple drive configuration refers to the direct connection between the motor and the pump. This arrangement eliminates the need for complex transmission systems and ensures efficient energy transfer between the motor and the impeller. The simplified mechanical structure improves reliability and reduces maintenance requirements in industrial environments.
Key Design Features of Centrifugal Couple Drive Chemical Process Pumps
Chemical process pumps must operate under demanding conditions where fluids may be corrosive, abrasive, or reactive. To address these challenges, centrifugal couple drive pumps incorporate specialized design features that enhance durability and operational safety.
The pump casing is typically manufactured using corrosion-resistant materials such as stainless steel or specialized alloys. These materials help prevent chemical reactions between the fluid and pump components, ensuring long-term structural integrity. The impeller is also designed to withstand continuous exposure to aggressive liquids while maintaining stable hydraulic performance.
Sealing systems are another critical element in chemical process pump design. Industrial chemical transfer often requires leak-proof operation to prevent hazardous fluid escape. Mechanical seals are commonly used to maintain a secure barrier between the internal pumping chamber and the surrounding environment.
Other important features commonly associated with centrifugal couple drive chemical process pumps include:
- Precision-engineered impeller for efficient fluid movement
- Robust pump casing designed for chemical compatibility
- Reliable shaft sealing systems to prevent leakage
- Balanced hydraulic design for smooth operation
- Direct coupling between motor and pump for improved efficiency
These design elements contribute to stable pump performance across a wide range of industrial applications.
Role of Centrifugal Pumps in Chemical Processing Systems
Chemical manufacturing operations involve multiple stages of fluid transfer. Raw materials must be transported to reactors, intermediate fluids are transferred between processing units, and finished products must be moved to storage or packaging systems. Pumps act as the central mechanism supporting these fluid movement processes.
Centrifugal couple drive chemical process pumps are commonly integrated into chemical processing systems because they offer a balance of reliability, efficiency, and operational simplicity. Their design supports continuous fluid flow, which is essential in production environments where interruptions can affect productivity.
In addition to transferring liquids, these pumps often support critical operational functions such as circulation, mixing assistance, and cooling system operation. By maintaining stable fluid movement, the pump helps ensure consistent process conditions within the manufacturing system.
Industrial Applications of Centrifugal Couple Drive Chemical Process Pumps
Chemical process pumps are used across a wide range of industries that require controlled liquid transfer. Their design allows them to handle fluids with varying viscosities and chemical compositions while maintaining system stability.
Common industrial applications include:
- Chemical manufacturing plants
- Pharmaceutical production facilities
- Petrochemical processing systems
- Industrial water treatment operations
- Fertilizer and agrochemical production
- Dye and pigment manufacturing plants
- Process industries involving corrosive liquids
Each of these industries relies on consistent fluid transfer to maintain production continuity. Centrifugal couple drive chemical process pumps support these operations by enabling controlled liquid movement between processing units.
Importance of Material Compatibility in Chemical Pumping
Handling chemical fluids requires careful consideration of material compatibility. Many chemicals can react with metals or cause corrosion over time, which may compromise pump performance or create safety risks. For this reason, chemical process pumps are manufactured using materials specifically selected for compatibility with industrial chemicals.
Engineers evaluate the chemical composition, temperature, and concentration of process fluids before selecting pump materials. Stainless steel, high-grade alloys, and chemically resistant coatings are commonly used to ensure the pump can operate safely under challenging conditions.
Material compatibility plays an important role in maintaining operational safety and extending equipment lifespan. Proper material selection reduces the likelihood of corrosion-related damage and helps maintain reliable pump performance.
Operational Efficiency in Industrial Pump Systems
Efficiency is an important factor in industrial pumping systems because pumps often operate continuously as part of large-scale manufacturing processes. Centrifugal couple drive chemical process pumps are designed to deliver consistent fluid flow while maintaining efficient energy usage.
The direct coupling between the motor and pump helps reduce mechanical losses. By minimizing energy loss during transmission, the pump can achieve improved hydraulic efficiency. Efficient pump operation contributes to stable process conditions and helps reduce the overall energy demand of industrial fluid handling systems.
In many industrial facilities, multiple pumps operate simultaneously as part of integrated process networks. Maintaining efficient pump performance across these systems helps improve overall plant productivity while ensuring reliable operation.
Maintenance Considerations for Chemical Process Pumps
Industrial pumps require periodic inspection and maintenance to ensure long-term performance. Chemical process pumps are designed to simplify maintenance procedures while maintaining operational reliability.
Routine maintenance activities may include inspecting seals, checking impeller condition, verifying alignment between motor and pump components, and monitoring vibration levels. These inspections help identify potential issues before they lead to system failure.
Maintenance planning is an essential part of pump management in chemical processing environments. By implementing structured maintenance schedules, facilities can maintain stable pump operation and minimize unexpected downtime.
Future Trends in Industrial Chemical Pumping Technology
Industrial pumping technology continues to evolve as manufacturing processes become more advanced. Modern chemical processing facilities require pumps capable of handling increasingly complex fluids while maintaining operational efficiency.
Advances in pump design, materials engineering, and monitoring technologies are contributing to improved pump performance. Innovations such as improved sealing systems, enhanced corrosion resistance, and advanced monitoring sensors are helping industrial operators maintain reliable fluid transfer systems.
As industrial production continues to expand, the demand for dependable pumping solutions will remain strong. Centrifugal couple drive chemical process pumps will continue to play a significant role in supporting safe and efficient chemical handling processes across a wide range of industries.
Centrifugal Couple Drive Chemical Process Pumps
Centrifugal couple drive chemical process pumps are essential components in industrial fluid handling systems where reliable liquid transfer is required. Their centrifugal operating principle, combined with direct motor coupling, enables efficient energy transmission and stable fluid movement across processing systems.
Industries that depend on consistent chemical transfer rely on these pumps to maintain production continuity while ensuring safe handling of process fluids. Their robust construction, corrosion-resistant materials, and efficient hydraulic design make them suitable for demanding industrial environments.
As chemical processing technologies continue to advance, dependable pumping systems will remain central to industrial operations. Centrifugal couple drive chemical process pumps will continue to support modern manufacturing systems by enabling controlled and efficient fluid transfer within complex production networks.
Frequently Asked Questions
Our Blogs
- Acids Transfer PVDF Chemical Pump
- Air Cooled Pump Set
- Thermic Fluid Hot Oil Air Cooled Pump
- Air Operated Double Diaphragm SS 316 Pump
- AODD Pump PVDF MOC
- Centrifugal End Suction Pump
- High Pressure Centrifugal Pump
- Vertical Centrifugal Pump
- Hygienic Centrifugal Pump
- Petroleum Industry Centrifugal Process Pump
- Self Priming Boiler Feed Pump
- Bare Shaft PP Pump
- Self Priming Monoblock Mud Pump
- Hot Oil Centrifugal Pump
- Horizontal Centrifugal Back Pull Out Bare Shaft Coupled Pump
- Teflon Line Centrifugal Process Pump
- Corrosion Resistant Pump
- Semi Open Impeller Centrifugal Pump
- Corrosion Resistant Polypropylene Pump
- Boiler Feed Pump
- 20 LPM Oil Gear Pump
- PVDF Loading Unloading Centrifugal Pump
- Vertical Extended Shaft Slurry Pump
- Pneumatic Air Operated Double Diaphragm Pump
- CF Series Stainless Steel Centrifugal Pump
- Oil Transfer Rotary Gear Pump
- High Temperature Pump
- Horizontal Centrifugal End Suction Pump
- Sewage Plants Self Priming Mud Pump
- Caustic Vertical Pump
- Polypropylene Gland Less Pump
- 300 LPM Acid Pump
- Single Stage Centrifugal Back Pull Out Pump
- Water Treatment Centrifugal Back Pull Out Pump
- Vertical Extended Shaft Sump Pump
- Horizontal Slurry Pump
- Mechanical Diaphragm Dosing Pump
- 2 HP Centrifugal Pump
- Vertical Long Shaft Sump Pump
- Stainless Steel Pump
- Centrifugal Circulation Process Pump
- Thermic Fluid Hot Oil Pump
- Self Priming Non Clog SS 316 Mud Pump
- Vertical Long Shaft Submerged Centrifugal Pump
- High Pressure Multi Stage Boiler Feed Pump
- Vertical Sump Pump
- Side Suction Pump
- Polypropylene Descaling Pump
- Non Clog Impeller Pump
- High Discharge Pump
- Filter Press Feeding Pump
- Polypropylene Chemical Process Pump
- Magnetic Drive Polypropylene Pump
- Water Circulation Pump
- Non Metallic Pump
- Side Suction Bare Shaft Pump
- SS 304 Centrifugal Fabricated Pump
- SS316 Rotary Gear Pump
- Centrifugal Flameproof Pump
- Corrosion Resistant PVDF Chemical Pump
- Centrifugal Pump Closed Impeller
- Stainless Steel Centrifugal Pump
- Corrosion Resistant PP Pump
- Heavy Duty Rotary Gear Pump
- External Gear Pump
- SS 316 AODD Pump
- Self Priming Non Clog Mud Pump
- Hot Oil Circulation Pump
- Internal Gear Pump
- Pneumatic Double Diaphragm Pump
- Thermic Fluid Boiler Feed Pump
- Magnetic Chemical Pump
- ETP Slurry Pump
- Filter Press Feed Pump
- Water Transfer Pump
- PVDF Lined Chemical Process Pump
- Industrial Chemical Process Pump
- SS Chemical Transfer Pump
- Vertical Single Stage Centrifugal Pump
- Hot Oil Circulation Pump in India
- Centrifugal Pump Manufacturers & Suppliers in India
- Chemical Process Pump Manufacturer in India
- Horizontal Single Stage Centrifugal Pump
- Self Priming Stainless Steel Pump
- Rotary Gear SS 316 Pump
- PVDF Chemical Pump in India
- PP AODD Pump
- PP Chemical Process Pump
- Vertical Long Shaft Sump Pump
- Air Cooled Thermic Fluid Hot Oil Pump
- Centrifugal Chemical Process Pump
- Air Operated Diaphragm Pneumatic Pump
- Industrial AODD Pump
- SS Air Operated Diaphragm Pump
- Air Cooled Pump Manufacturer & Supplier in India
- AIR COOLED HOT OIL PUMP
- PP Air Operated Double Diaphragm Pumps
- Vertical Inline Single Stage Centrifugal Pump
- Magnetic Drive Acid Handling Pump
- PVDF LINED CENTRIFUGAL PUMP
- Horizontal Single Stage Centrifugal Pumps
- SS 316 Pumps Centrifugal Chemical Transfer
- Pvdf Chemical Process Pump
- Self Priming Stainless Steel Pump in india
- SS TWIN LOBE PUMP
- SS ROTARY GEAR PUMP
- HOT OIL AIRCOOLED PUMP
- SS CENTRIFUGAL PUMPS IN INDIA
- SS GEAR PUMP IN INDIA
- PVDF MAGNATIC DRIVE PUMP
- Filter Press Side Suction Pump
- CHEMICAL PROCESS PUMP
- CENTRIFUGAL COUPLED PUMP
- THERMIC FLUIED AIR COOLED PUMP
- Lobe Pump in India
- SS Self Priming Mud Pump in Gujarat
- Solvent Transfer Pump in Gujarat
- PVDF Centrifugal Pump in Ahmedabad
- Rotary Lobe Pump in Ahmedabad
- End Suction Pumps Gujarat
- SS Centrifugal Pump in Gujarat
- Solvent Transfer Pump in Ahmedabad
- Vertical Seal Less Gland Less PP Pump in Ahmedabad
- VERTICAL SEAL LESS GLAND LESS PP PUMP
- PP SELF PRIMING PUMP
- SOLVENT TRANSFER PUMP
- SS CENTRIFUGAL PUMP
- ROTARY GEAR PUMP
- CENTRIFUGAL PP PUMP
- CHEMICAL PROCESS CENTRIFUGAL PUMP
- ROTARY LOBE PUMP
- Filter Press Side Suction Pump in Gujarat
- Air Cooled Thermic Fluid Pump in India
- SS Centrifugal Monoblock Pump in Ahmedabad
- MAGNATIC DRIVE CENTRIFUGAL PUMP
- ACID APPLICATION PUMP
- AIR OPERATED DOUBLE DIAPHRAGAM PUMP
- LOBE PUMP
- HORIZONTAL CENTRIFUGAL PUMP
- SS GEAR PUMP
- FIRE FIGHITING PUMPS
- FILLTER PRESS PUMP
- BACK PULL OUT SS CENTRIFUGAL PUMP
- PP SELF PRIMING PUMP
- Horizontal Back Pull Out End Suction Pumps in India
- Hot Oil Pump in Gujarat
- PVDF Centrifugal Pump in Gujarat
- Centrifugal Pump
- Thermic Fluid Air Cool Pump
- PP Pump
- PVDF Centrifugal Pump Manufacturers in Gujarat
- End Suction Pumps in Ahmedabad
- Bentonite Pumps in Gujarat
- SS SELF PRIMING MUD PUMP
- PP MONOBLOCK PUMP
- SS CENTRIFUGAL MONOBLOCK PUMP
- LOBE PUMP
- FILLTER PRESS SIDE SUCTION PUMP
- HOT OIL PUMP
- AIR COOLED THERMIC FLUID PUMP
- PVDF CENTRIFUGAL PUMP MANUFACTURERS IN AHMEMDABAD
- Magnetic Drive PP Pump
- Horizontal Back Pull Out End Suction Pumps in Gujarat
- Bentonite Pumps in Gujarat
- AIR OPERATED DIAPHRAGAM PUMP
- MAGNATIC DRIVE PP PUMP
- Rotary Gear Pumps
- PVDF CENTRIFUGAL PUMP
- End Suction Pumps in Gujarat
- Centrifugal Process Pump in Ahmedabad
- Horizontal Back Pull Out End Suction Pumps Manufacturer in Ahmedabad
- Bentonite Pumps Manufacturer in Ahmedabad
- Chemical Process Centrifugal Pump Supplier in Ahmedabad
- End Suction Pumps
- Centrifugal Process Pump
- Horizontal Back Pull Out End Suction Pumps
- Chemical Process Centrifugal Pump
- BENTONITE PUMPS
- Pp Centrifugal Acidic Liquid Transfer Pump
- Centrifugal Process Pump For Evaporators
- Polypropylene Aodd Pump
- PP Centrifugal Monoblock Pump
- Self Priming Mud Pump in Ahmedabad
- Rotary Gear Pump Supplier in Ahmedabad
- AODD Pump in Ahmedabad
- PP Monoblock Pump in Ahmedabad
- Centrifugal Couple Drive Chemical Process Pump
- SS 316 Pumps Centrifugal Chemical Transfer in Ahmedabad
- Eva Operation Pump
- Air Operated Double Diaphragm Pump Manufacturer in Ahmedabad
- Industrial Mud Pump Manufacturer in Ahmedabad
- AODD Pump Supplier in Gujarat
- Self Priming Mud Pump in Gujarat
- PP Monoblock Pump Supplier in Ahmedabad
- PP Centrifugal Pump Manufacturer in India
- Chemical Transfer Pump Supplier in Gujarat
- End Suction Pump Manufacturer in Ahmedabad
- Centrifugal Back Pull Out Pump Manufacturer in India
- SS Centrifugal Pump Manufacturing Company in Gujarat
- SS Gear Pump Supplier in Ahmedabad
- Rotary Gear Pump Manufacturer in India
- Flange Mounted Rotary Gear Pump Manufacturer in India
- Horizontal Centrifugal Pump Supplier in Gujarat
- Acid Transfer Pump Manufacturer in India
- Multistage Boiler Feed Pump Manufacturing in Gujarat
- Polypropylene Pump in India
- Chemical Process Pump in Ahmedabad
- High Pressure Multistage Boiler Feed Pump in Gujarat
- Vertical Inline Centrifugal Pump in Ahmedabad
- Magnetic Drive Pumps in Ahmedabad
- Lobe Pump in Ahmedabad
- PP Monoblock Pump Supplier in India
- PP Centrifugal Pump Manufacturer in Ahmedabad
- Chemical Transfer Pump Supplier in India
- End Suction Pump Manufacturer in Gujarat
- Centrifugal Back Pull Out Pump in Gujarat
- SS Centrifugal Pump Manufacturer in India
- SS Gear Pump Manufacturer in Gujarat
- Hot Oil Pump in ahemdabad
- Air Cooled Thermic Fluid Pump Manufacturer in Gujarat
- Air Cooled Pump Manufacturer in Gujarat
- Rotary Gear Pump Manufacturer in Ahmedabad
- Bentonite Pump Manufacturer in India
- Centrifugal Back Pull Out Pump Manufacturer in Ahmedabad