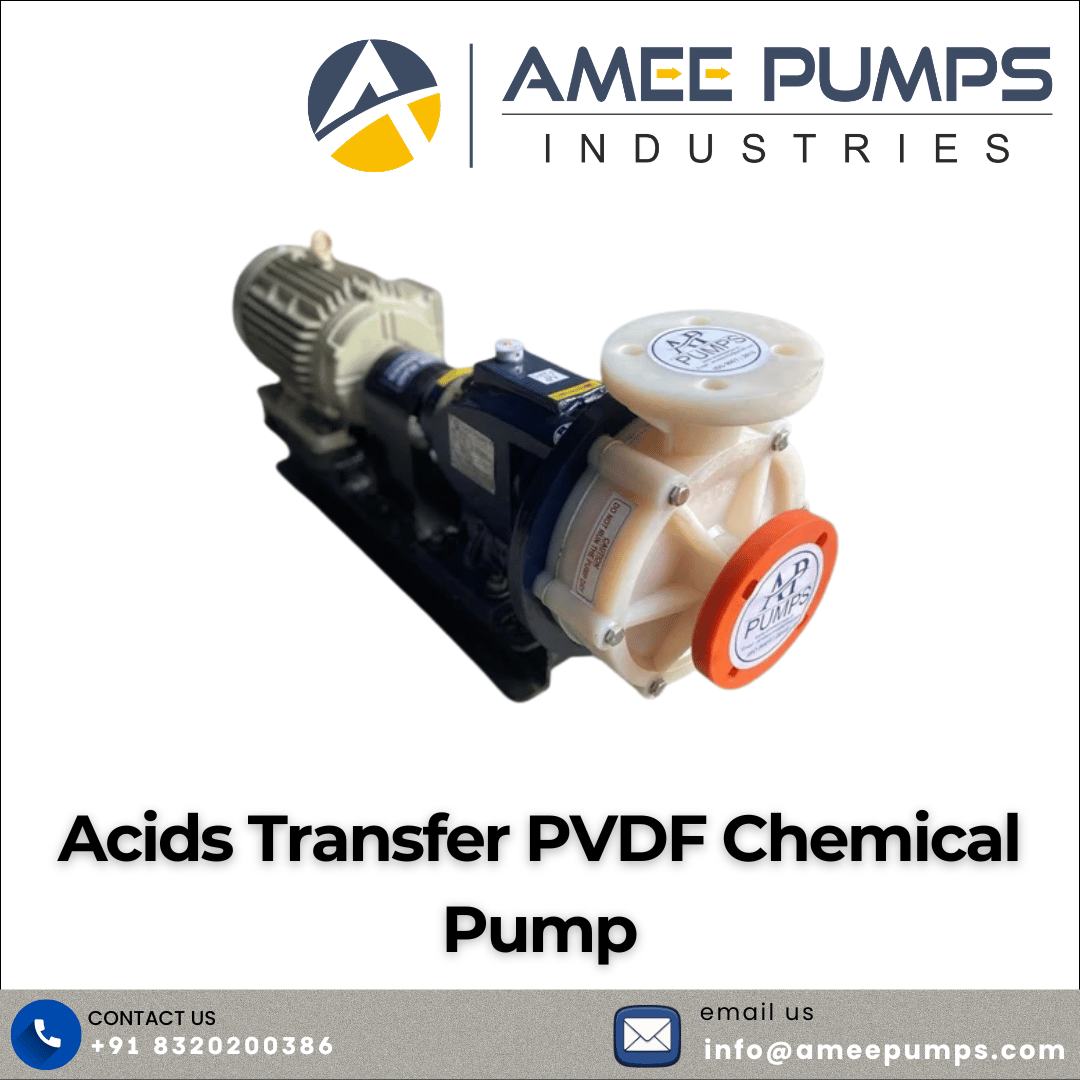
Acids Transfer PVDF Chemical Pump
Handling corrosive acids and aggressive chemicals demands equipment engineered for extreme resilience and safety. The Acids Transfer PVDF Chemical Pump stands at the forefront of this challenge, offering a robust solution for industries where fluid integrity and operational security are paramount. AMEE PUMPS INDUSTRIES leverages advanced material science and engineering expertise to deliver pumps that not only withstand harsh chemical environments but also ensure efficient and reliable fluid transfer.
This guide delves into the specifics of PVDF chemical pumps, their unparalleled advantages, diverse applications, and the critical factors to consider when selecting the right unit for your unique operational demands. We will explore how the inherent properties of PVDF, combined with intelligent pump design, provide a superior solution for transferring acids and other aggressive media, ensuring process continuity and plant safety.
Understanding the Necessity of PVDF Chemical Pumps for Acid Transfer
The transfer of acids and other highly corrosive chemicals presents significant challenges in industrial settings. Traditional pump materials can degrade rapidly when exposed to such aggressive substances, leading to equipment failure, costly downtime, potential environmental hazards, and safety risks for personnel. Polyvinylidene Fluoride (PVDF) has emerged as a material of choice for these demanding applications due to its exceptional chemical resistance, thermal stability, and mechanical strength.
PVDF pumps are specifically engineered to overcome the limitations of conventional materials. They offer a reliable barrier against a wide spectrum of corrosive fluids, including strong acids like sulfuric acid, hydrochloric acid, and nitric acid, as well as various organic and inorganic chemicals. This makes them indispensable in sectors such as chemical processing, pharmaceuticals, electroplating, semiconductor manufacturing, water treatment, and petrochemicals. AMEE PUMPS INDUSTRIES, with its foundation built on a tech-driven approach and decades of industry expertise, focuses on designing and manufacturing PVDF pumps that meet and exceed these stringent requirements.
Diverse Applications of Acids Transfer PVDF Chemical Pumps
The versatility and resilience of PVDF pumps make them suitable for a broad range of demanding applications across various industries:
Chemical Processing
Safely transferring concentrated acids, bases, solvents, and other corrosive reagents in synthesis, purification, and formulation processes.
Pharmaceuticals
Handling sensitive and aggressive chemicals during drug manufacturing, ensuring product purity and preventing contamination.
Electroplating & Surface Treatment
Circulating and transferring aggressive plating baths and pickling acids without material degradation.
Semiconductor Manufacturing
Managing ultra-pure or corrosive chemicals used in wafer cleaning, etching, and processing where material inertness is critical.
Water Treatment
Dosing and transferring treatment chemicals, acids for pH adjustment, and handling wastewater streams containing corrosive contaminants.
Petrochemicals
Transferring various corrosive hydrocarbons, additives, and process fluids in refining and chemical production.
Key Advantages of Utilizing PVDF Chemical Pumps
Choosing a PVDF chemical pump, particularly from a reputable manufacturer like AMEE PUMPS INDUSTRIES, brings substantial operational advantages:
- Exceptional Chemical Resistance: PVDF offers superior resistance to a broad range of acids, bases, solvents, and halogens, ensuring longevity even in aggressive media.
- High Thermal Stability: These pumps can operate effectively at elevated temperatures, typically up to 95–110 °C, without compromising structural integrity or performance.
- Mechanical Strength and Abrasion Resistance: PVDF provides high mechanical strength and is resistant to abrasion, allowing it to handle fluids with moderate particulate content.
- Leak-Free Operation (Magnetic Drive Options): Magnetic drive PVDF pumps eliminate the need for mechanical seals, drastically reducing the risk of leaks, emissions, and the associated maintenance, making them ideal for hazardous fluids.
- Durability and Reduced Maintenance: The inherent material properties translate to longer service life and reduced frequency of maintenance compared to pumps made from less resistant materials.
- Cost-Effectiveness: While the initial investment might be higher than for standard pumps, the extended lifespan, reduced downtime, and lower maintenance costs make PVDF pumps a highly cost-effective solution in the long run. AMEE PUMPS INDUSTRIES focuses on precision design to optimize performance and longevity.
Selecting the Right Acids Transfer PVDF Chemical Pump
Choosing the appropriate PVDF chemical pump involves careful consideration of several factors to ensure optimal performance and safety:
Crucial Selection Criteria:
- Fluid Characteristics: Identify the specific chemical composition, concentration, temperature, and viscosity of the fluid to be transferred.
- Flow Rate and Head Requirements: Determine the necessary flow rate (e.g., liters per minute or gallons per minute) and the total head the pump needs to overcome.
- Operating Temperature: Ensure the pump material and design can withstand the maximum operating temperature of the process.
- System Pressure: Verify the pump's pressure handling capabilities align with the system's maximum operating pressure.
- Sealing Requirements: For highly hazardous or valuable fluids, consider magnetic drive sealless pumps to prevent any potential leakage.
- Environmental Conditions: Assess the ambient conditions where the pump will be installed, considering factors like temperature, humidity, and exposure to corrosive fumes.
- Regulatory Compliance: Ensure the selected pump meets any industry-specific standards or environmental regulations.
Buyer Insight:
Don't underestimate the importance of understanding the long-term operational costs. While initial price is a factor, the total cost of ownership, including energy consumption, maintenance, and potential downtime, is a more accurate measure of a pump's true value. A well-selected PVDF pump from a quality manufacturer significantly reduces these long-term expenses.
Questions to Ask Before Buying:
Before finalizing your purchase, consider asking these questions:
What is the specific PVDF grade used in the pump construction?
Different PVDF grades can offer varying levels of performance. Understanding the material specifications ensures compatibility with your specific chemical application.
What are the maximum operating temperature and pressure limits for this specific model?
Confirming these limits against your process requirements is crucial for safe and reliable operation.
Does the pump design incorporate features to minimize wear and maximize efficiency?
Inquire about impeller design, bearing systems, and hydraulic efficiency to ensure long-term performance.
What are the recommended maintenance intervals and procedures?
Understanding maintenance needs helps in planning operational schedules and ensuring the longevity of the pump.
Can the pump be configured with a magnetic drive for sealless operation?
If leak-free operation is critical, inquire about the availability and benefits of sealless magnetic drive options.
Your Trusted Partner for PVDF Chemical Pumps: AMEE PUMPS INDUSTRIES
Founded in 2009 and led by Mr. Amit Panchal, who brings two decades of profound expertise in the pump industry, AMEE PUMPS INDUSTRIES is dedicated to advancing pump technology. Our approach is rooted in precision engineering and a tech-driven design philosophy, enabling us to deliver highly effective and cost-efficient solutions for the most challenging fluid transfer applications. We pride ourselves on a commitment to quality and customer satisfaction, striving for a 100% success rate on every project.
AMEE PUMPS INDUSTRIES offers a specialized range of PVDF Chemical Process Pumps designed for the safe and efficient handling of highly corrosive chemicals and aggressive fluids. Our focus on innovation ensures that each pump is built for optimal performance, reliability, and durability, meeting the stringent demands of modern industrial processes. We understand the critical nature of acid transfer and are committed to providing solutions that ensure operational continuity and safety for our clients.
Frequently Asked Questions about PVDF Chemical Pumps
What makes PVDF material ideal for pumping acids?
PVDF (Polyvinylidene Fluoride) is exceptionally resistant to a wide range of aggressive chemicals, including strong acids, and maintains its structural integrity at elevated temperatures, making it perfect for acid transfer applications where other materials would fail.
Can PVDF pumps handle solids or abrasive particles?
PVDF possesses good mechanical strength and abrasion resistance. While not designed for heavy slurries, PVDF pumps can generally handle fluids with moderate particulate content. Specific design considerations may be needed for highly abrasive applications.
What is the main advantage of a magnetic drive PVDF pump?
Magnetic drive PVDF pumps are sealless, meaning they do not have a mechanical seal. This design eliminates the primary point of leakage, making them extremely safe for hazardous or corrosive chemicals, and reduces maintenance associated with seal wear.
How does AMEE PUMPS INDUSTRIES ensure the quality of its PVDF pumps?
AMEE PUMPS INDUSTRIES employs a tech-driven approach to pump design and manufacturing, focusing on precision to ensure each pump delivers reliable performance. Our commitment is to provide top-notch, cost-effective solutions with a focus on achieving a 100% success rate in meeting client requirements.
What industries commonly use PVDF chemical pumps for acid transfer?
Industries such as chemical processing, pharmaceuticals, electroplating, semiconductor manufacturing, water treatment, and petrochemicals widely utilize PVDF pumps for handling corrosive acids and chemicals.
Request Your Customized PVDF Chemical Pump Solution
Ensure the safety, efficiency, and reliability of your acid transfer operations. Contact AMEE PUMPS INDUSTRIES today to discuss your specific requirements and get a tailored solution.
Get a Quote